
A crescent-shaped wear scar appeared on the port plate after 500-hour bench runs, with the block supplier and pump maker blaming each other.
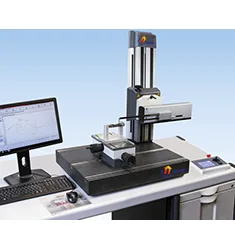
Solution: Ra, Rz and Rmr(30%) curves were taken at several bore depths with the CX-3/160, including the 15° chamfer transition, on new and run-in parts.
Result: Rmr(30%) in the chamfer fell from 62% to 41% — the pressure concentration was the root cause. Two-stage honing plus chamfer polishing cut the 500-hour scar depth by 70%.


