
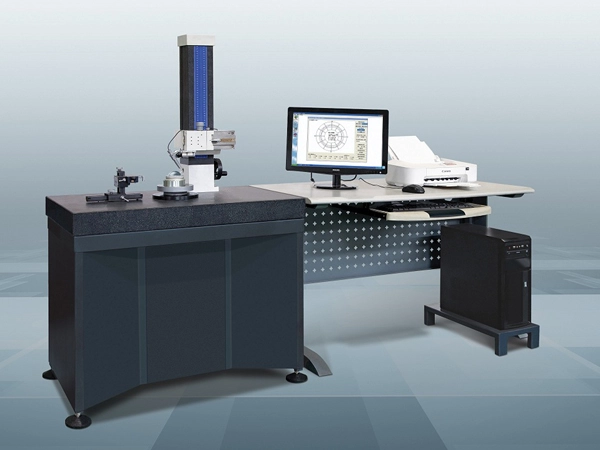
Servo valve spools run in sleeves with 2-3 um clearance; 0.5 um of roundness error can cause sticking. Outsourced metrology took three days, so the shop controlled lapping by feel, and outgoing sticking reached 1.2%.
Solution: a Y9025B roundness tester installed in a shop-floor temperature-controlled corner, with 0.025 um air-spindle accuracy, grading working-edge roundness, cylindricity and coaxiality per GB/T 7235. Five sections per spool, 50 UPR filter, 6 minutes per part.
Results: after match-lapping, spool roundness holds at 0.3 um and cylindricity at 0.6 um, with readings fed back to the lapping machine. Sticking dropped to 0.12%, outsourced metrology was eliminated, saving about 450000 yuan a year.


