
The aged hardness of C194 copper-alloy strip governs stamping burrs on lead frames. Lab Vickers checks ran weekly with results three days late, so off-hardness lots had often already stamped hundreds of thousands of pieces.
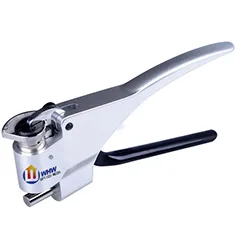
Solution: a W-B75 clamp-type Webster hardness tester (copper-alloy model) clamps 0.2-0.4 mm strip directly on the slitting line; three seconds per reading with a tiny indentation that does not affect downstream processing. An HW-to-HV conversion table goes out with the process documents, cross-checked against lab micro-Vickers data quarterly.
Result: in-line readings of 9.5-10.5 HW (about 125 HV) agreed with lab HV0.2 within 5%; one lot reading 0.8 HW low was intercepted immediately.
Benefit: hardness monitoring moved from weekly to every coil, and burr-related batch scrap has not recurred.


