
Gear shafts require 58–62 HRC at the surface and 30–42 HRC at the core after carburising and quenching. Manual Rockwell readings went onto paper and were typed into Excel the next day, so by the time an anomaly appeared hundreds of parts had been made.
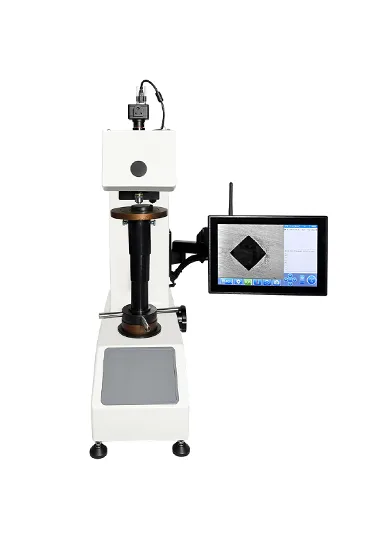
Solution: HRC-150SMJ digital motorised Rockwell with a V-block support; the operator loads the part and presses start for an automatic load-dwell-unload-read cycle in 18 seconds, with hardness, time, operator and part QR code written to MES over Ethernet.
Result: 18 seconds per part instead of 35, with all 40 samples per shift stored automatically; one 56.5 HRC reading triggered an immediate alarm and traced to quenching-oil temperature on furnace 3 within five minutes, avoiding about 600 reworked parts.


