
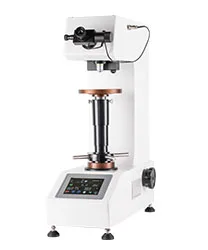
Wind-turbine hubs require 180–240 HBW in the body with wall thickness varying from 30 to 120 mm, so cooling rate differs by location. Testing a single point on a attached block did not represent the body, and customers demanded body measurements.
Solution: HBRVS-187.5 in Brinell mode at HBW 2.5/187.5 with a portable grinding station; six points per casting (flange, hub wall, fillet, two each), recorded and plotted as a gradient map.
Result: eight minutes per casting; the initial 22 HBW spread pointed to slow cooling in thick sections and fell to 11 HBW after chills were repositioned; conversion to tensile strength is within 12 MPa, fast enough to decide whether destructive sampling is needed.


