
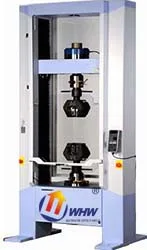
After press-fitting, the tie-rod ball pin must demonstrate a pull-out force of at least 30 kN. The simple hydraulic puller only showed the peak value, hiding press-fit disturbances, and the OEM PPAP demanded process curves.
Solution: an AGS-X13 benchtop electronic universal testing machine, 50 kN class 0.5, with a dedicated ball-pin pull-out fixture. The program pulls at 10 mm/min, records the full force-displacement curve, and judges peak and yield knee automatically with archiving.
Result: 40 seconds per piece with pull-out forces of 36-42 kN; one double-peak curve anomaly was traced to press hydraulic-pressure fluctuation, keeping 2000 suspect parts from shipping.
Benefit: curve traceability satisfied the OEM PPAP requirement, and the line moved smoothly from pilot build to mass production.


