
Joint efficiency of TC4 load-frame EB welds fluctuated between 0.88 and 0.95, failing to stably meet the 0.92 design floor; the link between weld microstructure and parameters was missing.
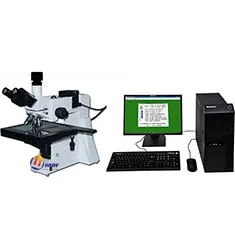
Solution: the MMAS-12 research microscope (incident/transmitted light) rated weld sections per HB 5276, measuring α-lath width and basketweave fraction at 500X across six focus-current settings.
Result: excessive focus current coarsened α laths (2.8 μm average) and caused the strength scatter. After optimization, lath width was 1.6 μm, joint efficiency stabilized at 0.96, and production yield reached 100%.


