
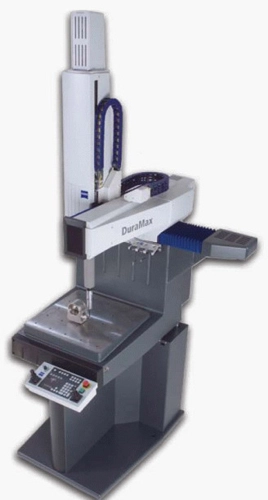
The plant makes 12000 e-drive housings a month with 0.04 mm coaxiality between stator bore and bearing seats. The metrology lab sampled five parts per shift, so drift was often found only after two shifts of bad parts had run - a 380000-yuan monthly scrap loss.
Solution: a DuraMax shop-floor CMM installed beside the machining line, with active temperature compensation over 15-40°C and a passive anti-vibration base against press vibration. Eighteen critical dimensions - stator bore, bearing seats, sealing face - run as a full-inspection program with robotic loading at a 6-minute cycle.
Results: 100% inspection of critical dimensions with SPC trends fed straight to the line, giving drift warnings two shifts earlier. Monthly scrap fell below 60000 yuan and customer PPM dropped from 850 to 120.


