
HXZMP-3000 Smart fully automatic metallographic grinder-polisher
Complete metallographic specimen preparation
- Control双盘磨抛,压力/转速/时间可编程
- Cooling循环冷却,试样温度可控
 HXGXS · 2026-11-17 · +86 21 5748 2007
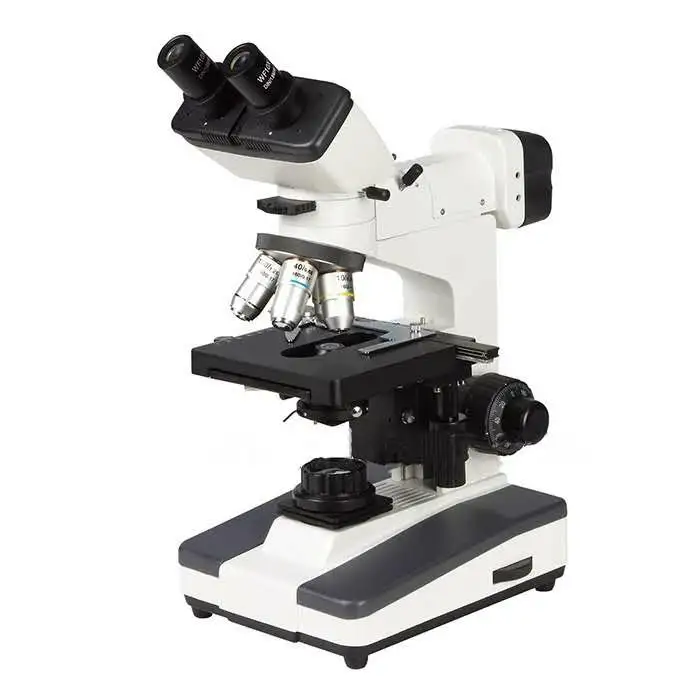
Complete metallographic specimen preparation
By submitting you agree to our privacy policy.
The HXGXS provides programmable, repeatable metallographic specimen preparation.
The HXGXS provides programmable, repeatable metallographic specimen preparation.
| Software | 晶粒度/层深/夹杂物评级,GB/T 6394、GB/T 10561 |
|---|---|
| Control | 适配 HX 系列金相显微镜与工业相机 |
| Profile parameters | 报告导出、标定与数据库管理 |
* Generated by rule engine over the product database; for pre-selection only.
The goal of metallographic preparation is a flat, scratch-free mirror with intact edges and unchanged microstructure. The sequence is sectioning → mounting → grinding → polishing → etching, and every step affects the result.
Sectioning: diamond or alumina wheels with constant feed and abundant coolant to avoid heat-affected zones and deformation. Soft materials use resin-bonded wheels, hard materials metal-bonded diamond.
Mounting: hot mounting (phenolic, 130–180 °C, 20–30 MPa) is fast; cold mounting (epoxy/acrylic) suits temperature-sensitive materials and edge retention; copper-filled mounts allow electrolytic polishing.
Grinding and polishing: remove scratches step by step, each step fully erasing the previous one; diamond suspension 3 µm then 1 µm, final oxide polish. Soft materials need low pressure and short times to avoid relief.
1. Grinding allowance: each grade must remove 3–4× the previous scratch depth — 20–30 µm per grade (320→1200) for carbon steel; rotate the sample 90° at each change.
2. Burn-free cutting: keep feed low enough that chips do not blue (~300 °C); burned layers shift surface hardness by 2–5 HRC and show as tempered zones.
3. Hot mounting: phenolic at 150–165 °C, 250–300 bar, 5–8 min; use cold epoxy (24 °C/24 h or accelerated 60 °C/1 h) for quenched or aluminium parts.
4. Polishing time: removal ∝ P·n; typical 2–3 min at 3 µm diamond and 1–2 min at 1 µm — excess pressure causes smearing and pitting.
5. Etching quota: 4% nital 3–8 s for carbon steel; fix time, temperature and concentration per batch for comparability.
| Standard | Title | Use |
|---|---|---|
| ASTM E3-11 | Guide for metallographic specimen preparation | Preparation workflow |
| GB/T 13298-2015 | Examination of microstructure | General inspection |
| GB/T 15749-2008 | Quantitative metallography | Quantitative analysis |
| GB/T 10561-2005 | Non-metallic inclusion content in steel | Inclusions |
| ISO 4967 | Determination of non-metallic inclusions | Export projects |
1. Four linked steps: sectioning without deformation, mounting without voids and with edge protection, polishing without scratches or rounding, then etching and observation. A wrong choice at any step cannot be rescued by a better microscope.
2. Cutter by section size and heat sensitivity: abrasive cutters (HXQ-50/HXQ-100) for routine parts; low-speed precision sectioning with diamond or CBN wheels below 300 rpm for coatings, sheet and non-ferrous.
3. Mounting by batch and edge requirements: hot mounting (HXZDQ) is fast and cheap for routine parts; cold vacuum impregnation suits porous, coated and electronic samples.
4. Polishing by throughput: manual (HXZMP-1000) below 20 samples a day, semi-automatic (HXZMP-2000) for 20–80, automatic heads (HXZMP-3000) above 80 or where consistency matters.
5. Consumables matter more than the machine: grit sequence 180→400→800→1200→2000, diamond suspension 9→3→1 µm and the right cloth type must match, or you either cannot polish out or polish past the feature.
6. Room and safety: extraction and water for cutting and polishing, separate preparation and microscopy rooms, guards and e-stops on cutters.
| Equipment | Model | Capability | Use |
|---|---|---|---|
| Precision cutter | HXQ-50 / HXQ-100 | Low speed, no deformation | Coatings, sheet, non-ferrous |
| Abrasive cutter | HXGXS | Fast large-section cutting | Routine steel parts |
| Hot mounting press | HXZDQ-100 / 110 / 120 / 160 | Φ25–Φ50 mounts | Batch routine samples |
| Vacuum mounting | HXZDQ-100Z | Vacuum impregnation | Porous, coated, electronics |
| Manual polisher | HXZMP-1000 | Single platen | Low volume, teaching |
| Semi-automatic | HXZMP-2000 / 2000Z | Twin platen, timed | Medium batches |
| Automatic | HXZMP-3000 | Multi-station, programmable force | High throughput, consistency |
| Electrolytic polish/etch | HXSQ-100G / 100F | Deformation-free surface | Stainless, nickel alloys |
Why samples get scrapped: cutting heat alters the structure, mounting gaps cause edge smearing, over-polishing removes inclusions, over-etching blurs grain boundaries.
Sampling. Choose a representative section (gear root, weld cross-section), cut perpendicular to the viewing plane, and record position and orientation.
Cutting. 0.5–2 mm/min feed, 2000–3000 rpm, abundant coolant; re-section if burn marks appear.
Mounting. Hot mount at 150 °C, 25 MPa for 8 min; cold epoxy cure 4 h (or 60 °C acceleration). Add a protective plate for coating cross-sections to prevent rounding.
Grinding and polishing. 320→600→800→1200, rinse and rotate 90° between steps; diamond 3 µm (3 min), 1 µm (2 min), oxide (1 min), decreasing force.
Check. Inspect unetched at 100× for scratches and edge rounding, then etch. Verify preparation quality daily with a reference sample.
Complete metallographic specimen preparation

Complete metallographic specimen preparation

Complete metallographic specimen preparation
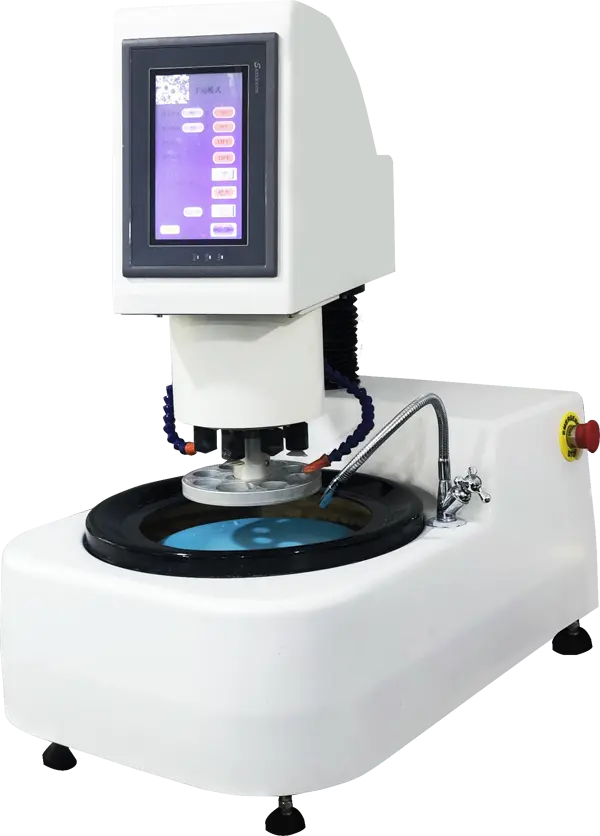
Complete metallographic specimen preparation