 HOT
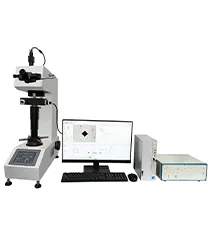
HMAS-D5/10/30/50SZA Vickers Hardness Tester
Vickers Hardness Tester
- 测量分析系统HMAS‑硬度测量分析系统
- 光学成像系统维氏硬度大三通光学成像系统
 YHRI-150SM · 2026-11-17 · +86 21 5748 2007
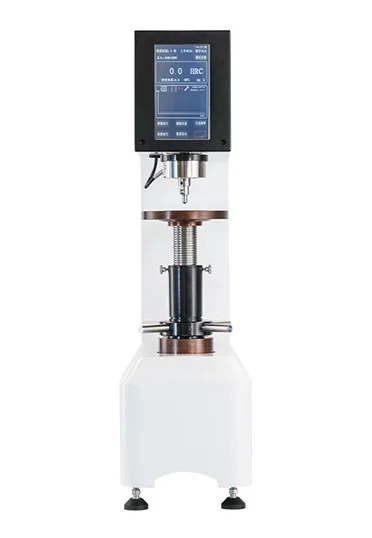
Rockwell Hardness Tester
By submitting you agree to our privacy policy.
YHRI-150SM传感器数显全洛氏硬度计属于自动型洛氏硬度计,外观新颖,触摸屏幕操作和显示,菜单式结构,采用传感器加载,硬度值以数字直接显示.硬度测试结果可以直接打印输出,
自动化程度高,消除了操作和读数误差。简便了硬度之间的硬度换算等功能。
适用于金属材料的洛氏硬度试验。本系列洛氏硬度计操作简便迅速,性能稳定,使用广泛。可进行黑色金属和有色金属的洛氏硬度测定,广泛适用于工厂车间和计量部门。
二、产品特点:
1、闭环传感器控制系统,无需砝码;
2、无需特殊安装,甚至无需售后;
3、测量精度高;
4、硬度标尺选择时,提示选用压头;
5、实验力可定做,结构简单。
产品型号
YHRI-150SM
操作方式
触摸屏
加载机构
高精度传感器加载
测量标尺
HRA、HRBW、HRC、HRD、HREW、HRFW、HRGW、HRHW、HRKW、HRLW、HRMW、HRPW、HRRW、HRSW、HRVW、HR15N、HR30N、HR45N、HR15TW、HR30TW、HR45TW、HR15WW、HR30WW、HR45WW、HR15XW、HR30XW、HR45XW、HR15YW、HR30YW、HR45YW
硬度测量范围
洛氏:HRA:20 ~ 88,HRB:20 ~ 100,HRC:20 ~ 70表面洛氏:HR15N:70 ~ 91、HR30N:42 ~
80、HR45N:20 ~ 70、HR15T:73 ~ 93、HR30T:43 ~ 82、HR45T:12 ~ 72
转换标尺
HRA、HRB、HRC、HRD、HRF、HBW、HV、HK、HR15N、HR30N、HR45N、HR15T、HR30T、HR45T
总试验力
15Kg(147.1N)、30Kg(294.2N)、45Kg(441.3N)、588N(60kgf)、980N(100kgf)、1471N(150kgf)
执行国家标准
GB/T230.2 国家标准,JJG112 检定规程
试验力保持时间 (s)
3 种试验力保荷满足特殊材料使用。
初试验力保荷时间
机器设定 0-60s,最小变动量 1s
总试验力保荷时间
机器设定 0-60s,最小变动量 1s
初试验力返回保荷时间
机器设定 0-60s,最小变动量 1s
计算方式
自动计算
硬度分辨率
0.1HR
试件最大高度
175mm
压头中心距离
160mm
丝杆直径
外径 φ40mm
大平台直径
φ150mm
中平台直径
φ55mm
V 型台尺寸
φ35mm
数据输出
内置微型打印机
电源电压
AC 220V/50Hz
外形尺寸
540*215*750mm(长*宽*高)
净重
90.5kg
毛重
110.5kg
YHRI-150SM Rockwell Hardness Tester supplied by CHWES. 0 key specifications available on request.
* Generated by rule engine over the product database; for pre-selection only.
Hardness testing presses an indenter into the surface under a constant load and converts indentation size or depth into a hardness value. Vickers uses a 136° diamond pyramid: HV = 0.1891 × F(N)/d²(mm), where d is the mean diagonal.
Hot hardness is performed in vacuum or high-purity inert gas. Specimen and indenter are heated independently and must be at the same temperature or corrected per the standard; loading, dwell and unloading all happen inside the hot zone, and the indentation is measured through a high-temperature optic or after cooling. The HMAS series uses a uniform hot zone with ±5 °C uniformity from 200 to 1600 °C.
1. Rockwell: HR = K − h/0.002 (K = 100 for HRC, 130 for HRB). At h = 0.078 mm, HRC = 61.
2. Brinell: HBW = 2F/(πD(D−√(D²−d²))); with F=1838.6 N, D=2.5 mm, d=1.1 mm, HBW ≈ 192.
3. Vickers: HV = 0.1891·F/d² (F in N); F=9.807 N with d=0.05 mm gives HV ≈ 742.
4. Test forces: choose Brinell loads by 0.045F/D²; Rockwell 10 kgf preliminary with 60/100/150 kgf total; surface scales 3 / 15/30/45 kgf.
5. Conversions: HRC ≈ HBW/10 only as a rough mid-range guide — official reports must follow the GB/T 1172 tables.
| Standard | Title | Scope |
|---|---|---|
| GB/T 4340.1-2009 | Vickers hardness test — test method | Vickers |
| GB/T 230.1-2018 | Rockwell hardness test | Rockwell |
| GB/T 231.1-2018 | Brinell hardness test | Brinell |
| ISO 6507-1 | Vickers hardness test | Export |
| ASTM E92 | Vickers hardness of metallic materials | Americas |
| GB/T 17394.1-2014 | Leeb hardness test | Portable |
Hot hardness has no unified national standard; ASTM E92 practice is normally cited with temperature, atmosphere, dwell and indenter material stated in the report.
1. Principle follows the target: Rockwell for macro hardness and heat-treatment acceptance; Brinell for cast iron, annealed and forged parts where a large indent is representative; Vickers or micro-Vickers for thin layers, coatings and small areas.
2. Bench or portable: bench units (HRC-150SMJ, HBRVS-187.5) where parts can be brought in; portable Leeb for large moulds, in-service piping and non-removable parts, corrected against a bench reference, typically within ±2 HRC.
3. One for many: mixed, low-volume shops do well with a Brinell-Vickers-Rockwell combination unit covering HRA/HRB/HRC/HV/HB.
4. Automation: manual below 100 parts per operator per day; motorised elevation, automatic loading and data upload (HRC-150SMJ) above 200 or for unattended runs.
5. Reference blocks: two to three blocks covering the working range, checked every shift and sent for annual calibration.
6. Specimen requirements: Rockwell needs thickness at least ten times the indent depth and Ra ≤1.6 µm; otherwise switch to Vickers or superficial Rockwell.
| Model | Principle | Range | Typical use |
|---|---|---|---|
| HRC-150SMJ | Rockwell, motorised digital | HRA/HRB/HRC | Batch sampling in heat treatment |
| HRC-150SM / HRC-150M | Rockwell | HRA/HRB/HRC | Incoming and in-process checks |
| HRC-45M | Superficial Rockwell | 15N/30N/45N | Sheet, plating, case layers |
| HRS-150M / XHRS-150M | Digital Rockwell | HRA/HRB/HRC | Lines needing data upload |
| HBRVS-187.5 | Brinell-Vickers-Rockwell | HBW/HRA/HRB/HRC/HV | Mixed low-volume production |
Three rules for trustworthy data: check the reference block every shift and record it; keep the support face flat and clean; keep indent spacing at least three indent diameters.
Specimen. Test and support faces parallel; thickness at least 1.5 × diagonal (Vickers) or 10 × depth (Rockwell); Ra ≤ 0.4 µm, free of scale and oil.
Room temperature. Select load, apply within 10–15 s, dwell 10–15 s, unload, measure diagonals. Spacing between indentations ≥3d, from the edge ≥2.5d.
Hot hardness. Load the specimen, evacuate or backfill argon, ramp and soak 20–30 min, lower the indenter, load and dwell, unload, cool or measure hot, then apply the temperature correction.
Gradient. Step every 0.05–0.1 mm to the hardness plateau; determine effective case depth at 550 HV1 per GB/T 9450.
Quality control. Check a certified block (e.g. 700 HV1) each shift, recalibrate beyond ±3%, and log furnace curves and atmosphere for hot tests.
HOTVickers Hardness Tester
 HOT
Vickers Hardness Tester
 HOT
Micro Vickers Hardness Tester
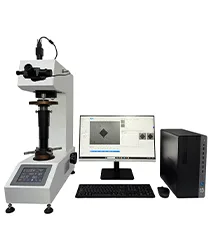
Vickers Hardness Tester · M