
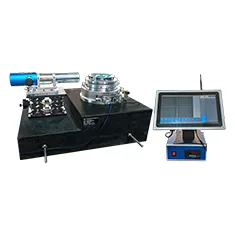
The hydrostatic tables were rated ±3 arcsec, but the machine tool builder measured out-of-tolerance indexing at acceptance, and the two parties disputed the reference.
Solution: MC030-ZJQFCJY-1 with a grade-0 24-face polygon verifies indexing bidirectionally every 15° over 0-360° per JJG 472, separating indexing error from mounting eccentricity.
Result: maximum indexing error was 2.6 arcsec, and 0.8 arcsec of it came from coupling eccentricity. With the compensation table written into the CNC, closed-loop accuracy stably reaches ±1 arcsec and acceptance passed at first attempt.


