
The side outer panel measures 1.6 m by 1.1 m with more than 60 assembly holes. Go/no-go gauges on the checking fixture only gave pass/fail with no deviation values, so die correction relied on veteran experience and new-model tryout needed many rework loops.
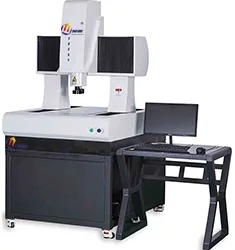
Solution: a YR8060-M large-travel gantry vision machine with 0.5 µm scales and stitched measurement, holding ±8 µm indication error over 1 m. The coordinate system is built on RPS points, every hole gets an X/Y deviation vector map, and the boundary is scanned against the CAD model.
Result: full vector maps in 12 minutes per panel; the die shop corrected dies directionally from the vectors, and after two loops the hole-position pass rate rose from 82% to 97%.
Benefit: a quantitative monitoring layer beyond the fixture cut tryout rework loops by about 40% and pulled SOP two weeks earlier.


