 HOT
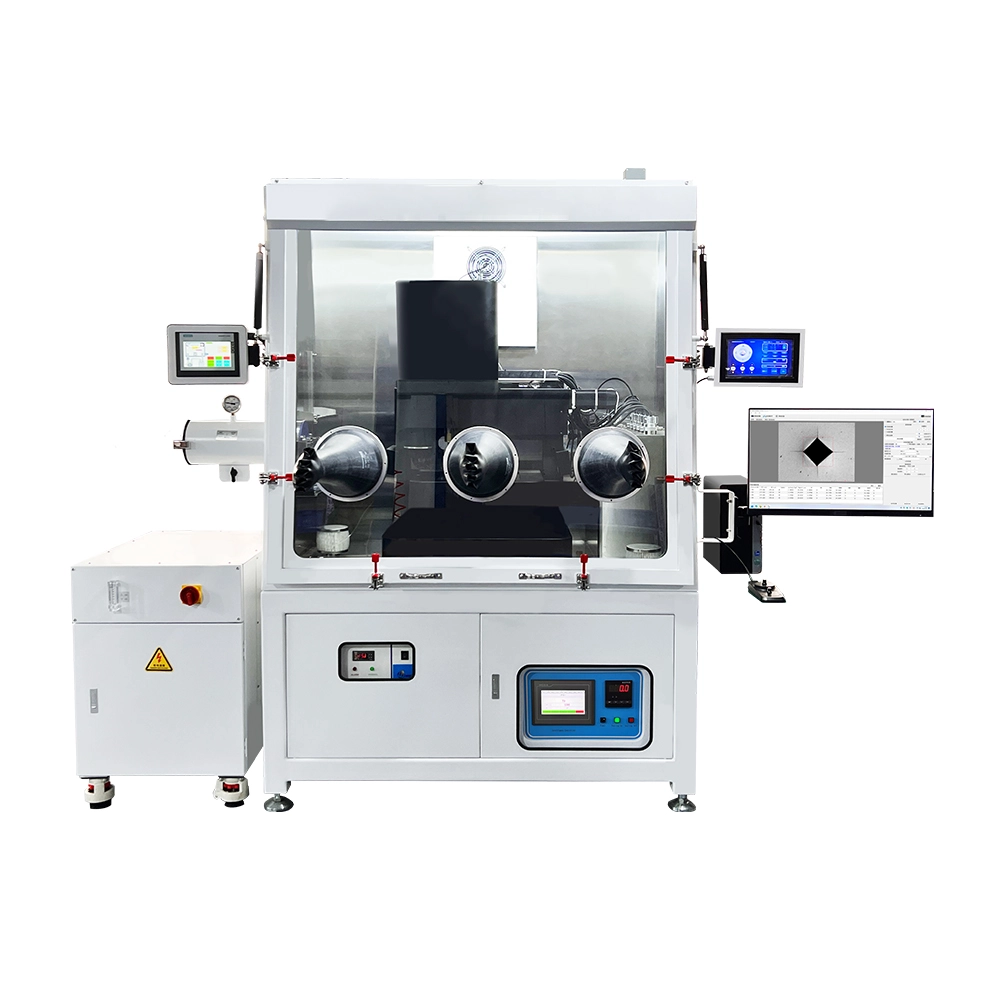
IMAS-HT900CM High-temperature Hardness Tester
High-temperature Hardness Tester
- 使用温度范围室温~800℃
- 炉腔温度范围≤900℃
 HMAS-HT800 · 2026-11-17 · +86 21 5748 2007
High-temperature Hardness Tester
By submitting you agree to our privacy policy.
HMAS-HT800用于室温~800℃材料性能研究,结合高温光学观察与定力值加载及自动加卸载。
以下为厂家原站标称参数。原文载荷单位kg保留,力值单位及可选项需在技术协议中确认;显示分辨率不等于测量准确度。
HMAS-HT800用于室温~800℃材料性能研究,结合高温光学观察与定力值加载及自动加卸载。
标配10X物镜,可选配20X物镜。完整参数表保留原站的标准配置与选配条件,载荷单位“kg”按原站记录,订购时需确认力值单位与校准范围。
测试温度范围、炉腔温度、压针预热温度及换样系统极限温度分别列示;各模块的极限值不能替代整机测试温度。
用于高温维氏硬度与压痕形貌分析。断裂韧性等派生量需选择适合材料与裂纹形态的评价方法,不能仅由产品配置认定方法有效。
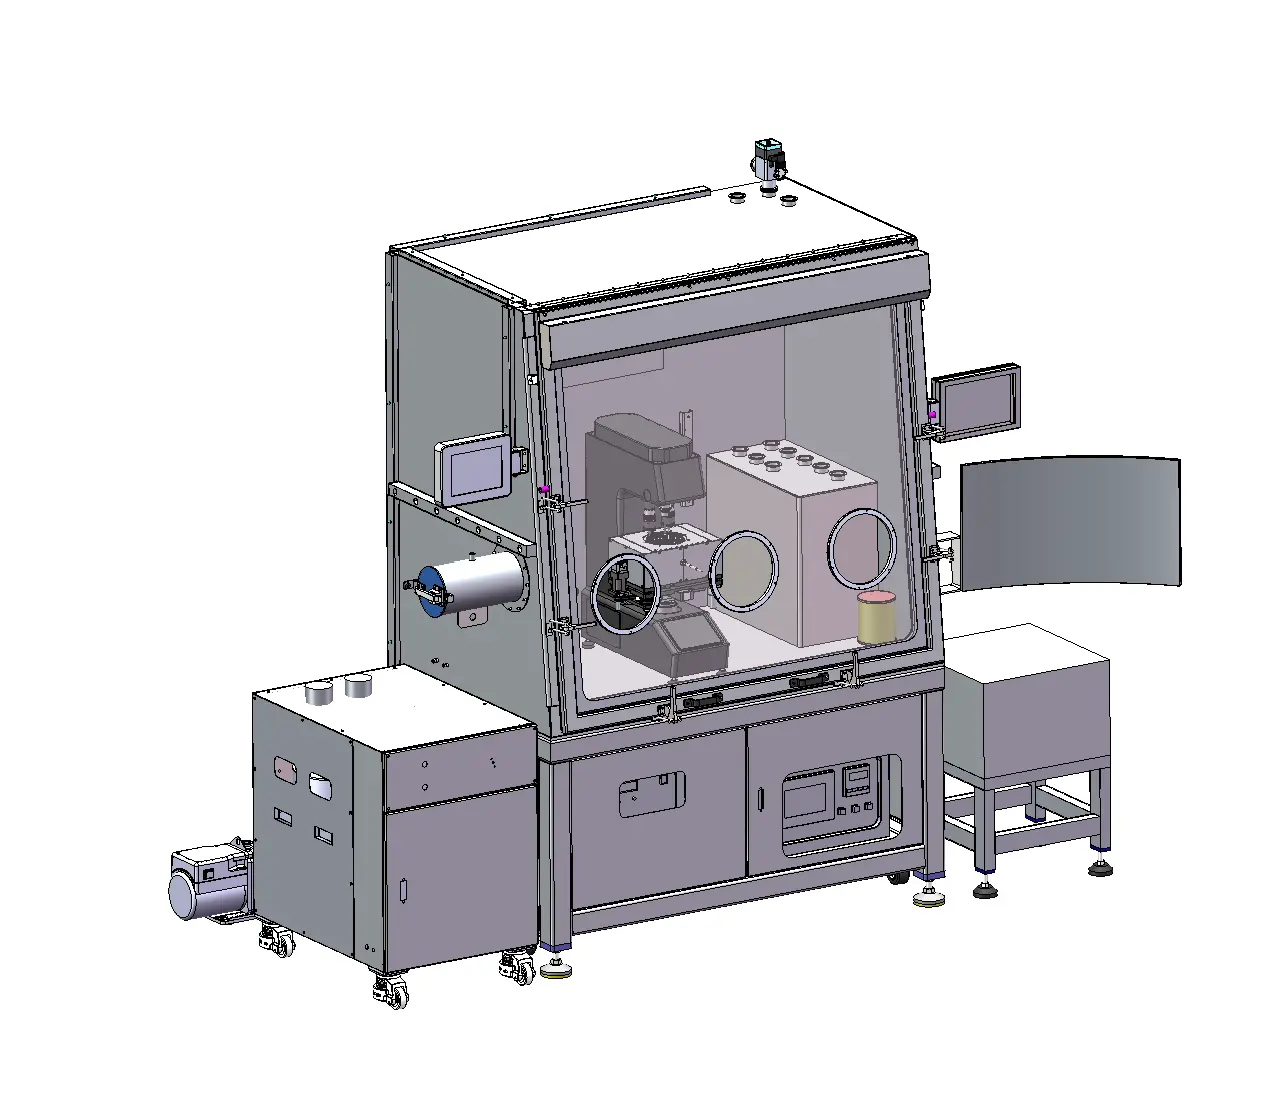
全温场的含义是:加热炉、压针、物镜、加载机构与换样机构处在同一个温度场里。试样从装炉到压痕观察完成都不离开炉腔,不需要“加热—取出—冷却—再测量”,因此氧化、脱碳与组织转变不会被误读成材料本身的温度响应。
硬度形成链:压针在设定力值下压入试样表面并保荷,卸载后由物镜在同一温度场直接观察压痕,测量对角线 d,按 HV = 0.1891·F/d² 计算维氏硬度(F 单位 N,d 单位 mm)。力—时间原始曲线与压痕图像同时存档,用于复核与追溯。
温度链:HRE高温合金 加热,S型热电偶 测温,温控精度 ≤±0.3℃,温场梯度 ≤±5℃,升温速率 1–40℃/min。炉腔显示温度、试样附近温度与压针预热温度分别记录;炉腔上限 800℃ 是炉体能力,不等于可测温度 800℃。
光学与运动链:10X 物镜(选配 20X),物镜工作温度 ≤800℃,系统显示放大 1000X(选配 2000X),物镜分辨率 1.44 μm(选配 1.19 μm);多轴联动定位精度 ≤±1 μm,使“压入—观察—换点”在同一温度场里连续完成。分辨率是成像能力,不能当作测量准确度。
以 1 kgf(9.80665 N)载荷、压痕对角线 0.050 mm 为例:HV = 0.1891 × 9.80665 ÷ 0.050² ≈ 742。这是公式演示,不代表本机在该载荷下的实测值或不确定度。
hP P maxh max S = dP/dh hold (creep) 暂停动画重播force-depth力—位移曲线:加载段斜率、保荷段深度增长与卸载初始斜率分别对应弹性响应、时间相关变形与接触刚度。 动图为原理示意,曲线与数值非仪器实测数据。02 / CONFIGURATION仪器主要构成以下为本系列公开的模块构成,具体配置以技术协议为准;标注“选配”的项目不作为标准供货。
HMAS-HT800 High-temperature Hardness Tester supplied by CHWES. 53 key specifications available on request.
| 使用温度范围 | 室温~800℃ |
|---|---|
| 炉腔温度范围 | ≤800℃ |
| 温控精度 | ≤±0.3℃ |
| 温度场梯度误差 | ≤±5℃ |
| 升温速率范围 | 1℃~40℃/min |
| 炉腔温场尺寸 | 80*80*60mm |
| 试样尺寸 | ≤φ20*20mm |
| 加热元件 | HRE高温合金 |
| 控温热电偶 | S型热电偶 |
| 加载力值范围 | 1~30kg |
| 力值档位 | 固定16档位,选配32、61、127档 |
| 加载方式 | 定力值 |
| 定力值加载精度 | ≤1kg时±2%;>1kg时±0.5% |
| 定力值加载分辨率 | 0.01%FS |
| 保荷时间 | ≤30min |
| 传感器 | 力值传感器 |
| 预热时长 | ≤30min |
| 预热时间 | 自定义,单位min或s |
| 最高预热温度 | ≤800℃ |
| 物镜放大倍数 | 10X物镜(选配20X物镜) |
| 系统显示放大倍数 | 1000X(选配2000X) |
| 物镜分辨率 | 1.44um,选配1.19um |
| 更换方式 | 自动 |
| 更换时长 | ≤20秒 |
| 联动轴数 | 4轴 |
| 运动控制精度 | ≤±1.5um |
| 运动控制速度 | ≤5000um/s |
| 运动控制分辨率 | ≤0.1um |
| 运动控制方式 | 自动 |
| X轴行程 | 15mm |
| Y轴行程 | 15mm |
| Z轴行程 | 60mm |
| Z-A轴行程(样品) | 50mm |
| Z-B轴行程(压针) | 20mm |
| 最大流量 | 13L/min |
| 介质 | 惰性气体 |
| 冷却时间 | ≤10秒 |
| 冷却组数 | 4 |
| 冷却角 | 90° |
| 材质 | 立方氮化硼CBN、接杆为镍铬合金 |
| 镍铬合金总长 | 110mm |
| 是否可修复 | 否 |
| 选配可修复全尺寸1700型压针 | 110mm*φ8(可选配110mm*φ6.35) |
| 水氧指标 | ≤1ppm |
| 工位数 | 1.0 |
| 尺寸 | 2200*1420*2270mm |
| 腔室尺寸 | 1350*950*1400mm |
| 箱体材质 | 304不锈钢 |
| 箱体底板材质 | 304不锈钢 |
| 额定制冷量 | 1050W |
| 制冷剂 | R134a |
| 温度范围 | 15~36℃ |
| 噪音 | ≤63dB(A) |
* Generated by rule engine over the product database; for pre-selection only.
HMAS/IMAS full-temperature instruments bring loading, optics and temperature control to the hot end simultaneously:
The IMAS indenters add instrumented loading (ISO 14577), deriving hot modulus and hardness from force–displacement curves by the Oliver-Pharr method.
1. Vickers: HV = 1.8544·F/d² (F in kgf, mean diagonal d in mm); F = 1 kgf with d = 0.06 mm gives HV ≈ 515. Ceramics at 1600 °C typically need 1–5 kgf.
2. Loading accuracy: ±2% below 1 kg, ±0.5% above, 0.01% FS resolution; the force-time slope yields the loading rate.
3. Instrumented indentation (Oliver-Pharr): stiffness S = dP/dh from the top third of unload; hc = hmax − 0.75Pmax/S; Ac = 24.5hc²; H = Pmax/Ac; Er = (√π/2)S/√Ac, with E solved from the compliance relation.
4. Hot fracture toughness: KIC = 0.016(E/H)1/2F/c3/2; with E/H = 20, F = 10 kgf, c = 0.15 mm, KIC ≈ 4.1 MPa·m1/2.
5. Creep: fit the hold segment displacement for the strain rate ε̇ = dh/dt/hc to judge microstructural stability.
| Standard | Title | Scope |
|---|---|---|
| GB/T 4340.1-2009 | Metallic materials — Vickers hardness test, Part 1 | Indentation measurement |
| ASTM E92-17 | Vickers and Knoop hardness | Acceptance testing |
| ASTM E384-17 | Microindentation hardness | Micro/small-force indents |
| ISO 14577-1:2015 | Instrumented indentation test, Part 1 | IMAS modulus/hardness |
| ISO 14577 series | High-temperature indentation annex guidance | Hot-stage traceability |
Record temperature points, soak time, atmosphere, raw force-time data and in-situ images for research-grade traceability.
1. Temperature first: take process temperature plus 20% headroom. 600 °C class: HMAS-HT600/HT700CM; 800 °C: HT800/HT900CM; 1200 °C: HT1200/HT1300CM; 1400 °C: HT1500CM; 1600 °C: HMAS-UHT1700CM or IMAS-UHT1700.
2. Hardness only or full curve: HMAS for Vickers indents and morphology; IMAS for force-displacement curves, hot modulus and creep compliance to ISO 14577.
3. Atmosphere drives configuration: TiAl, refractory metals and coatings need inert gas or vacuum (O₂ ≤10 ppm) with a glovebox; heat-resistant steels and cast irons run on high-purity argon.
4. Load by material: 0.1–10 kg for ceramics and thin coatings, 1–30 kg standard for superalloys and hardmetals, up to 150 kg for castings and forgings.
5. Production or research: 50 s same-field sample exchange and multi-station for line sampling; in-situ imaging, programmable temperature steps and full raw-data export for research.
6. Facility: ≥3.8×2.0×2.8 m footprint, 99.999% argon, 220 V / ≥6.5 kW, floor vibration ≤VC-C.
| Model range | Max temperature | Typical use | Key capability |
|---|---|---|---|
| HMAS-HT600 / HT700CM | 600–700 °C | Al/Cu alloys, tempered steel | Vickers indent + in-chamber imaging |
| HMAS-HT800 / HT900CM | 800–900 °C | Heat-resistant steel, cast iron, hardmetal | Long soak, batch exchange |
| HMAS-HT1200 / HT1300CM | 1200–1300 °C | Ni superalloys, TBC | Inert atmosphere, coating cross-sections |
| HMAS-HT1500CM | 1500 °C | Refractory alloys, ceramics | High vacuum, hot optics |
| HMAS-UHT1700CM / IMAS-UHT1700 | 1600–1700 °C | UHTC, single crystal, nuclear | Extreme chamber, in-situ curves |
| IMAS-HT700CM / HT900CM | 700–900 °C | Creep and modulus | ISO 14577 force-displacement |
What moves price and lead time: temperature ceiling, vacuum or glovebox, load range, in-situ imaging and thermal-conductivity ports, LIMS integration. Standard units ship in 45–60 days; 1600 °C and glovebox configurations need 90 days or more.
Specimens: ≤φ30×30 mm, parallelism ≤0.02 mm, measuring face Ra ≤0.4 µm (ideally ≤0.1 µm); transfer refractories inside the glovebox to avoid moisture pickup.
Temperature: verify with the type-B couple near the specimen; soak 15–30 min per point until gradients are within ±5 °C before loading.
Indenter: manage diamond life (≤50 h), keep one indenter per campaign, spacing indentations 3–4 diagonals apart.
Data: ≥3 valid indents per temperature, full force-time curves (plus displacement on IMAS); discard and photograph anomalous unloads (oxidation, spalling).
Checks: verify the loading chain on a certified block at 25 °C; quarterly high-temperature consistency runs with a reference ceramic.
HOTHigh-temperature Hardness Tester
 HOT
High-temperature Hardness Tester
 HOT
High-temperature Hardness Tester
High-temperature Hardness Tester