
Behind the 20±2 °C Rule: How Thermal Expansion Coefficients Feed CMM Temperature Compensation
Steel grows 11.5 μm per metre per degree; a 1 °C offset on a 500 mm part is 5.8 μm of error, so temperature compensation is not optional.
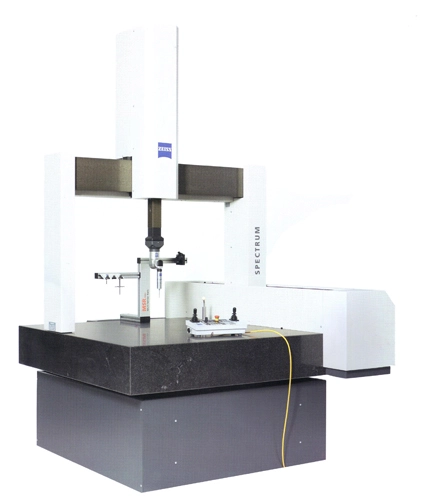
Origin of the 20 °C reference
ISO 1 fixes 20 °C as the reference temperature for geometrical quantities; every dimensional tolerance implicitly refers to 20 °C. Workpieces and machine scales expand and contract with temperature: steel at 11.5×10⁻⁶/K, aluminium at 23×10⁻⁶/K, granite beams about 6.5×10⁻⁶/K. Steel scales partially self-compensate steel parts, but an aluminium part on steel scales mismatches by 11.5 μm per metre per degree — the physical root of the 20±2 °C laboratory rule, ±1 °C at precision grade.
Error estimation
Uncompensated length error is ΔL=L·Δα·ΔT_machine + L·α_part·ΔT_part. Example: a 500 mm aluminium part at 23 °C on scales at 21 °C gives ΔL≈500×(23×10⁻⁶×3 - 11.5×10⁻⁶×1)≈28.7 μm. CMMs ship with temperature sensors, three on the machine scales and one or two on the part, and software folds each α back to 20 °C. Residual error after compensation depends mainly on sensor thermal contact and the accuracy of the entered α.
Gradients hurt more than averages
Temperature gradients bend structures: a 0.5 °C difference across the beam bends the guideways by several microns over one metre. Laboratory specifications therefore limit gradients as well — under 1 °C/h in time and 0.5 °C/m vertically. Parts need soaking after entering the room: a 100 kg steel part from a 30 °C shop needs 4-6 hours for the core to follow, and surface temperature alone is no proof of uniformity.
Practical checklist
- Attach the part sensor near the measured features with thermal grease;
- Enter the actual grade-specific α into the software; steel coefficients on aluminium parts are a classic blunder;
- Estimate soaking time at one hour per 50 kg as a floor for castings and weldments;
- Shop-floor CMMs lean on wide-band compensation, yet direct sunlight and HVAC blasts remain forbidden;
- State part temperature and compensation status in reports so referee re-measurement can reproduce conditions.


