 HOT
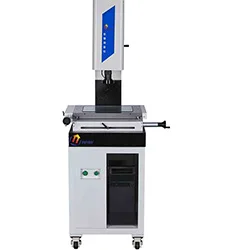
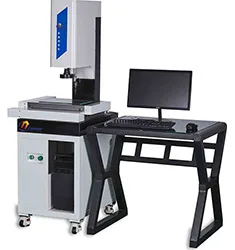
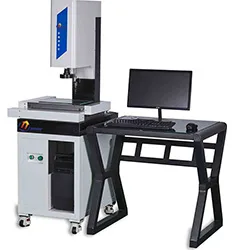
YR3020CNC-T CNC Vision Measuring Machine
CNC Vision Measuring Machine
- 测量工件尺寸300*200*180mm
- X/Y轴测量精度3+L/200um
 YR1010 · 2026-11-17 · +86 21 5748 2007
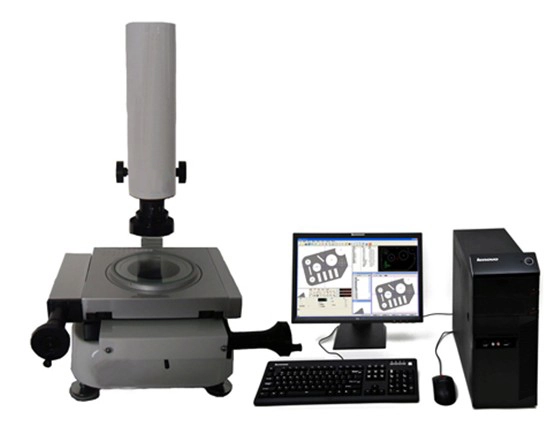
2D Vision Measuring Machine
By submitting you agree to our privacy policy.
影像测量仪
YR2010S 手动二次元影像测量仪
YR3020S 手动二次元影像测量仪
YR4030S 手动二次元影像测量仪
YR5040S 手动二次元影像测量仪
YR2010Z 自动聚焦二次元影像测量仪
YR3020Z 自动聚焦二次元影像测量仪
YR4030Z 自动聚焦二次元影像测量仪
YR5040Z 自动聚焦二次元影像测量仪
YR3020CNC CNC全自动二次元影像测量仪
YR4030CNC CNC全自动二次元影像测量仪
YR5040CNC CNC全自动二次元影像测量仪
YR3020CNC-T 探针型CNC全自动三次元影像测量仪
YR4030CNC-T 探针型CNC全自动三次元影像测量仪
YR5040CNC-T 探针型CNC全自动三次元影像测量仪
YR4030-M 龙门式全自动影像测量仪
YR5040-M 龙门式全自动影像测量仪
YR6050-M 龙门式全自动影像测量仪
YR8060-M 龙门式全自动影像测量仪
YR80100-M 龙门式全自动影像测量仪
YR120100-M 龙门式全自动影像测量仪
YR120150-M 龙门式全自动影像测量仪
YR1010 微型二次元影像测量仪
YR-T 经济型影像测量仪
YR-F 实用型影像测量仪
YR-W 卧式影像测量仪
YR-D 非接触三次元影像测量仪
YR-N 经济型自动影像测量仪
YR-C 承载型自动影像测量仪
YR-A 接触式三次元自动影像测量仪
YR-Q CNC智能化影像测量仪
YR-60I 批量检测型影像测量仪
YR-100I 批量检测型影像测量仪
YR-150I 批量检测型影像测量仪
投影仪
三坐标测量机
轮廓测量仪
圆度仪
洛氏硬度计
显微硬度计
维氏硬度计
布氏硬度计
邵氏硬度计/巴氏硬度计/韦氏硬度计
进口硬度计
硬度计耗材/配件
自准直仪
金相试样切割机
金相试样磨抛机
金相试样镶嵌机
金相试样预磨机/抛光机
光谱砂带磨样机/磨平机/电解抛光腐蚀仪
金相制样耗材
CMAS清洁度检测分析系统
MMAS科研级工业自动显微镜测量系统
IMAS复合材料断裂韧性残余应力检测仪
BMAS材料气泡测量分析系统
金相显微镜
体视显微镜
生物显微镜
偏光显微镜/荧光显微镜
其它显微镜(工具/比较/进口)
电子万能试验机
液压万能试验机
冲击试验机
光谱仪
元素分析仪/碳硫分析仪
色谱仪
光度计
探伤仪
粗糙度仪
测高仪
测厚仪
测温仪
测振仪
石油化工仪器
气体检测仪
食品仪器
内窥镜
3D打印设备
滴定仪/浊度计/水分测定仪
扭矩扳手/推拉力计
马弗炉/干燥箱/培养箱/试验箱
教学实训装置
熔点仪
旋光仪
折光仪/折射仪/糖度计/密度计/浓度仪
离心机/离心浓缩仪
滴点软化点测定仪/差示扫描量热仪
4008127833/021-58391850
扫一扫关注我们
硬度计案例 硬度计技术
试验机案例 试验机技术
金相制样案例 金相制样技术
自准直仪案例 自准直仪技术
显微镜案例 显微镜技术
实验室保养 实验室搬迁
研润简介 研润发展历程
人才与招聘
研润旗下产品及公司简介
维氏硬度计 洛氏硬度计 硬度计
自准直仪 拉力试验机 硬度计
万能试验机 金相抛光机 硬度计
金相切割机 金相切割机 硬度计
圆度仪 轮廓仪 硬度计 硬度计
自准直仪 自准直仪 硬度计
显微镜 金相显微镜 硬度计
金相切割机 影像测量仪 硬度计
布氏硬度计 自准直仪 金相磨抛机
硬度计 自准直仪 硬度计,金相切割机
上海研润光机科技有限公司成立于2005年,是
一家以研发、生产、非标定制自动化检测设备,
计算机软件开发为主的高新技术企业。主导产品
光学和材料性能仪器,包括硬度计、试验机、显
微镜、金相制样、工业自动化流水线定制、非标
自动化质量控制检验、工业机器人、高精度光学
自准直仪、残余应力测试、复合材料测试等设备。
YR1010 微型两次元影像测量仪
YR1010 2D Vision Measuring Machine supplied by CHWES. 0 key specifications available on request.
* Generated by rule engine over the product database; for pre-selection only.
Vision measuring systems replace contact metrology with imaging: backlight turns part edges into a high-contrast silhouette, while surface and coaxial light reveal bores, blind holes and steps. After capture, software extracts sub-pixel edges, fits lines, circles and arcs by least squares, establishes a part coordinate system (3-2-1 or best-fit) and computes distances, angles, concentricity and position tolerance.
The stage is driven by servo motors and precision screws with linear encoder feedback (0.1–1 µm). CNC models automate the move–capture–measure sequence for batch inspection. Accuracy is typically stated as U = 2.0 + L/200 µm at 20 ± 2 °C.
1. Indication error: commonly E = (2.5 + L/150) µm (L in mm); at L = 200 mm, E ≈ 3.83 µm, verified with a glass ruler along the diagonals.
2. Pixel size: field width ÷ active pixels; an 8 mm field on 1280 px gives 6.25 µm/px, improved to 1/10 px by sub-pixel algorithms.
3. Circle fit: σ(diameter) ≈ σpoint/√n — use ≥16 points per least-squares circle.
4. True position: deviation Δ = 2√(Δx² + Δy²) versus tolerance zone φt; Δx=0.02, Δy=0.015 mm gives Δ = 0.05 mm.
5. Thermal correction: 100 mm of steel changes 1.2 µm per °C (α≈11.5×10⁻⁶/°C) — apply on the shop floor.
| Standard | Title | Use |
|---|---|---|
| GB/T 24762-2009 | GPS — acceptance and reverification tests for imaging instruments | Acceptance, annual check |
| JJF 1318-2011 | Calibration specification for vision measuring instruments | Calibration |
| ISO 10360-7 | Acceptance tests for CMMs with imaging probing systems | Export projects |
| VDI/VDE 2617 | Accuracy of coordinate measuring machines | Accuracy rating |
| GB/T 1958-2017 | GPS — verification of geometrical tolerance | GD&T |
1. Calculate travel first: maximum part envelope plus fixture plus approach margin, then add 20%. Sizing on the part alone is the classic mistake. YRVMS covers 150×100 to 1200×1500; larger parts need YRVMS5030 or gantry models.
2. Three accuracy numbers, not one: indication error (E), repeatability (R) and scale resolution. E = 2.5+L/200 µm is standard, 1.8+L/300 µm for precision work; a 0.001 mm display means nothing on its own.
3. Manual, motorised or CNC: manual (YRVMS1510F) for sampling, motorised (YRVMS2010E and up) for repetitive batches, CNC (YRVMS3020CNC and up) for programmed multi-feature and unattended runs.
4. Optics and lighting decide capability: 0.7–4.5× zoom with bi-telecentric optics for planar dimensions; laser or touch probe for height, blind holes and deep slots; coaxial light for polished metal, backlight for transparent parts.
5. Software, three questions: can it build a coordinate system from drawing datums rather than by eye, does it output FAI/PPAP sheets, and does it support SPC and Excel export.
6. In-line inspection is a different machine: use YR-MV for cycle-time-driven 100% inspection instead of a measuring machine.
| Series | Drive | Travel (mm) | Typical use |
|---|---|---|---|
| YRVMS1510F | Manual | 150×100 | Small-part sampling, teaching |
| YRVMS2010E / 2515F | Motorised / manual | 200×100 / 250×150 | Connectors, precision hardware |
| YRVMS3020CNC / 4030CNC | CNC | 300×200 / 400×300 | 3C FAI, batch programming |
| YRVMS5030 / 5030CNC | CNC | 500×300 | Mid-size structural parts |
| YRVMS120150 | Gantry CNC | 1200×1500 | Sheet and large contours |
| YR-MV1080 / 7070 | Dedicated vision | Custom | In-line 100% inspection |
| YR-QVS series | Flash measurement | Small field | One-click multi-dimension |
Acceptance advice: verify E with a glass scale after installation, check R by measuring the same part ten times, then compare against a part with known CMM results; the deviation should stay within E.
Environment. 20 ± 2 °C, 40–60% RH, vibration-free; warm up 30 minutes; soak parts at least 2 hours (4 for large parts).
Calibration. Measure a glass scale or ceramic gauge block at near and far positions in X/Y/Z; perform ISO 10360-7 probing in seven directions with a length standard.
Measurement. Establish the coordinate system (plane–line–point or 3-2-1); take at least five points per feature (six for a circle, eight for a large circle); avoid chamfered edges; repeat each feature three times.
Verification. Check daily with a known artefact (50 mm block, certified circle); recalibrate when deviation exceeds one third of MPE.
Uncertainty. Dominated by temperature (11.5 × 10⁻⁶/°C × L), encoder error, edge algorithm and clamping repeatability; state U at k = 2.
HOTCNC Vision Measuring Machine
 HOT
CNC Vision Measuring Machine
 HOT
CNC Vision Measuring Machine